


CAS 58543-16-1 | Rebaudioside A (Stevia Extract) | 99% Purity Food Grade Sweetener | China Manufacturer
Natural zero-calorie sweetener for food, beverage, and specialty nutrition applications.
Rebaudioside A (CAS 58543-16-1) - Product Overview
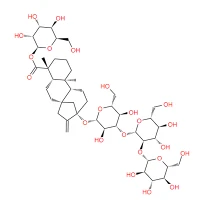
Stevia Extract (Rebaudioside A, CAS 58543-16-1, E960c) is a high-purity steviol glycoside extracted from the leaves of Stevia rebaudiana Bertoni. As a zero-calorie natural sweetener 200–300 times sweeter than sucrose, it is widely used in food, beverages, and tabletop sweeteners. For formulators, however, its real performance depends on one key metric: purity.
Standard stevia extracts often carry a bitter, metallic aftertaste due to residual non-Reb A glycosides. Alfa Chemical addresses this at the manufacturing level. We supply a strictly controlled ≥99.0% HPLC grade. At this purity, off-notes are minimized, allowing formulators to reduce or eliminate masking agents while achieving a cleaner sweetness profile.
We produce this grade at our facility in Zhengzhou, China, meeting JECFA and FDA GRAS standards. We supply from 25g bench-trial samples up to 25kg bulk drums, with batch-specific COA and SDS included with every order to simplify your procurement process.

High-purity Rebaudioside A crystalline powder (≥99% HPLC). Heat-stable up to 200°C. (Representative image; batch appearance may vary.)
Key Features Of Rebaudioside A
While Reb A is known for its intense sweetness, the real performance differentiator lies in its purity and stability. Here are the 7 core technical advantages for your formulation.
Applications: Food, Beverage & Specialty Nutrition
Reb A adapts across multiple matrices. Here are eight major applications and how Alfa Chemical addresses the specific formulation challenges in each.
Rebaudioside A vs Other Sweeteners
Why do formulators choose Reb A over traditional artificial sweeteners or sucrose? Here is the direct comparison.
* Comparison based on standard commercial grades. Alfa Chemical's ≥99% purity reduces the metallic aftertaste often associated with lower-grade stevia extracts.
Convinced by the data?
Test our ≥99% purity in your own lab. We provide 25g evaluation samples and batch-specific COAs.
Rebaudioside A Specifications
Detailed specifications for CAS 58543-16-1 Rebaudioside A are listed below. For batch-specific COA or SDS, please contact us.
| Item | Specification |
|---|---|
| Product Name | Rebaudioside A (Stevia Extract) |
| Synonym | Reb A; Steviol Glycoside; E960c |
| CAS Number | 58543-16-1 |
| EINECS | 611-696-6 |
| Molecular Formula | C44H70O23 |
| Molecular Weight | 967.01 g/mol |
| Purity (HPLC) | ≥99.0% |
| Appearance | White to off-white crystalline powder |
| Sweetness | 200–300× sucrose (zero calories) |
| Heat Stability | Up to 200 °C |
| pH Stability | 3–9 |
| Loss on Drying | ≤ 6.0% |
| Heavy Metals (as Pb) | ≤ 10 mg/kg |
| Total Plate Count | ≤ 1000 cfu/g |
| Yeast & Mold | ≤ 100 cfu/g |
| Storage | Cool, dry place in sealed container. Avoid moisture and direct sunlight. |
| Shelf Life | 24 months under proper storage conditions |
| Packaging | 25 g / 100 g / 500 g / 1 kg / 5 kg / 25 kg |
| Documents | COA, SDS |
| Manufacturer | Alfa Chemical (Zhengzhou, China) |
Quality Documentation For Rebaudioside A
Each batch of Rebaudioside A CAS 58543-16-1 is tested for:
Batch-specific COA for Rebaudioside A CAS 58543-16-1 available upon request. Safety Data Sheet (SDS) also available for download. Contact us for the latest batch test report.
Packaging & Shipping From China Manufacturer
📦 Packaging Options
25g / 100g / 500g / 1kg / 5kg / 25kg (custom packaging available)
✈️ Shipping Methods
International express courier for small quantities; air freight or sea freight for bulk orders
⏱️ Delivery Time
3-7 business days after payment confirmation
📄 Documentation
COA (Certificate of Analysis) and SDS (Safety Data Sheet) provided with every shipment
🏆 Why Buy Rebaudioside A From Alfa Chemical
We are a manufacturer, not a trading company. Alfa Chemical operates an integrated production facility in Zhengzhou, China. By controlling the entire supply chain-from raw material extraction to final packaging-we eliminate middleman markups, guarantee strict batch-to-batch consistency, and provide direct engineering support for your specific formulation needs.
Stock & Lead Time
Held in Zhengzhou. 25 g to 25 kg ship same week, bulk orders ship in 2–3 weeks.
Documentation
Batch-specific COA with every lot. Third-party testing can be arranged before shipment on request.
Factory Experience
Supplying food and beverage manufacturers since 2018. If you are new to stevia formulation, ask us - we will tell you what usually goes wrong.
Customization
If the ≥99.0% grade does not fit your process, tell us the purity or pack size you need. We can quote custom specifications.
Browse other pharmaceutical intermediates or send us your spec.
Frequently Asked Questions
Related Resources
About Alfa Chemical: Based in Zhengzhou, China, Alfa Chemical is a leading manufacturer and supplier of fine chemicals, biochemicals, and specialty intermediates. We serve food & beverage manufacturers, pharmaceutical companies, and research institutions worldwide with high-purity ingredients and reliable supply chain solutions.
Disclaimer: This product is intended for food, beverage, and industrial manufacturing use only. It is the buyer's responsibility to ensure that the product is used in compliance with all applicable local laws, regulations, and safety standards. All specifications are typical values and should be confirmed against the batch-specific Certificate of Analysis before use.
Hot Tags: CAS 58543-16-1 | Rebaudioside A | Alfa Chemical, China CAS 58543-16-1 | Rebaudioside A | Alfa Chemical manufacturers, factory, 2-Bromo-m-xylene, 3 deoxy adenosin, Pharmaceutical Intermediates, Cordycepin, Methyl toluenesulfonate, 4 Amino 4H 1 2 4 triazole


