


A practical formulation guide for R&D teams to overcome aqueous solubility limits, mask bitter aftertaste, and meet regulatory purity standards.

High-purity Rebaudioside A crystalline powder. The uniform particle size distribution supports rapid dissolution in hot-fill beverage lines. (Representative image; batch appearance may vary.)
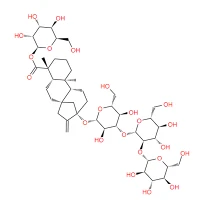
Rebaudioside A (Reb A, CAS 58543-16-1) is a high-purity steviol glycoside that is 200–300 times sweeter than sucrose. That number is the reason formulators reach for it. The reason they sometimes put it back on the shelf is different: at room temperature, Reb A does not dissolve easily enough for many beverage systems, and at higher use levels it brings a bitter aftertaste that sucrose never had.
This article is not a product overview. It is a formulation decision guide: where the solubility of this specific steviol glycoside actually limits you, how to manage the aftertaste without over-engineering the formula, and why the purity line is not just a marketing number - it is the regulatory entry ticket for most export markets.
In This Article
1. Solubility: The Real Constraint, Not the Sweetness
The sweetness of CAS 58543-16-1 is not the bottleneck. Its aqueous solubility is. In room-temperature water, Reb A dissolves to a limited extent, and the exact ceiling depends on temperature, pH, and the presence of other solutes. In concentrated beverage concentrates or syrup systems, this ceiling is reached faster than formulators expect.
The practical consequence is not that Reb A "doesn't work." It is that you cannot treat this steviol glycoside like sucrose in a concentrate. If the formula calls for a high sweetness load in a small volume, you either heat the aqueous phase, use a co-solvent system, or accept a lower concentrate strength.
If your process already includes a hot-fill or pasteurization step, the solubility window of Rebaudioside A widens. If you are formulating a cold-fill concentrate, solubility becomes the first variable to test - not the last.
2. Aftertaste: Manage It, Don't Mask It Blindly
Reb A's bitter aftertaste is concentration-dependent. At low use levels in a flavored system, it is often below the sensory threshold. At higher levels - or in neutral-pH systems with little flavor coverage - it becomes the dominant sensory note.
The common mistake is to throw a masking agent at the problem. A better sequence is: first, check whether the Reb A level can be reduced by blending with another sweetener; second, check whether the flavor system can carry the bitterness; third, consider a sweetness modulator. Masking without reducing the Reb A load often adds cost without solving the sensory issue.
Reb M and Reb D are frequently cited as "cleaner" alternatives, but both have their own solubility constraints. Swapping Reb A for Reb M is not a free upgrade; it trades one formulation problem for another.
3. The ≥95% Regulatory Threshold vs. ≥99% Commercial Grade
For food and beverage use, the relevant specifications are not vague. JECFA requires ≥95% total steviol glycosides on a dry basis for high-purity preparations. FDA GRAS conclusions for CAS 58543-16-1 have similarly centered on material at ≥95% purity.
This means a 90% extract is not simply "slightly less pure." For many export destinations and branded beverage customers, it falls outside the specification that the regulatory file was built on. The purity number is a procurement filter, not a preference.
Alfa Chemical supplies ≥99.0% (HPLC) grade Rebaudioside A - comfortably above the ≥95% regulatory floor. The commercial advantage of ≥99% is not only compliance safety; it means less non-Reb A glycoside load, which typically translates to a cleaner sweetness profile and less batch-to-batch sensory variation in beverage systems.
All values are typical; batch-specific data is provided on the COA. Final specification is confirmed upon order.
4. A Practical Decision Sequence for Reb A
If you are evaluating CAS 58543-16-1 for a beverage or food system, run the checks in this order:
1. Solubility first. Determine the maximum concentration your aqueous phase can hold at your actual process temperature. Do this before sensory work.
2. Sweetness load second. Set the target sweetness level with the solubility ceiling in mind. If the target cannot be met with Reb A alone, consider a blend before considering a different glycoside.
3. Aftertaste third. Evaluate bitterness at the actual use level in the final matrix, not in water. Flavor coverage changes the perception substantially.
4. Purity last, but before procurement. Confirm that the COA meets the ≥95% regulatory threshold required by your destination market, and the ≥99% specification required by your customer.
How Alfa Chemical Supports Reb A Formulation
Alfa Chemical manufactures high-purity Rebaudioside A at our Zhengzhou, China facility. The grade is positioned at ≥99.0% Reb A by HPLC, with batch-specific COA documentation covering actual assay, heavy metals, and residual solvents.
For formulation teams, the practical value is not just the purity number - it is the documentation that comes with it. If your project requires a specific purity window or a blend, the conversation starts from your target specification, not from a catalogue range.
For solubility or aftertaste questions at the bench stage, contact our technical team with your matrix and target use level. We provide 25g R&D samples directly from stock, with a typical lead time of 3–7 days.
Share this article: Rebaudioside A in Beverage Formulation: Managing Solubility, Aftertaste, and the Purity Threshold. Alfa Chemical R&D Formulation Team, November 2026. URL: https://www.alfa-industry.com/info/rebaudioside-a-in-beverage-formulation-managi-103728395.html
Further Reading
1. What Is Stevia? Rebaudioside A & Steviol Glycosides Guide An overview of Reb A structure, sweetness properties, and glycoside selection.
2. Rebaudioside A Safety: What the Evidence Actually Shows A plain-language review of JECFA, EFSA, and FDA assessments and steviol metabolism.
3. Rebaudioside A (CAS 58543-16-1) | ≥99% Specifications & Batch COA View full technical parameters, request a batch COA, or order an R&D sample.
Need a batch-specific COA for Rebaudioside A (CAS 58543-16-1)?
Send your target purity and application. Alfa Chemical replies within 12 hours.
Disclaimer: This article is for technical reference only. Solubility and sensory behavior depend on the specific matrix, pH, temperature, and co-ingredients. Final suitability should be confirmed by the user under actual process conditions. All purity values are typical reference ranges; batch-specific data is provided on the COA.